
Chemical supply shaped around your operation
Chemical solutions connected to the way your industry operates
We work with industrial customers whose requirements combine product specification with safe handling and dependable supply. Our chemical and logistics capabilities can be brought together around the particular needs of your site.
The right chemistry
Discuss the product, grade and concentration your process requires.

Fit for your site
Align packaging, storage and delivery with your receiving facilities.
Supply you can plan around
Coordinate distribution and replenishment with your consumption pattern.
Chemical supply tailored to your industry
We supply chemicals to customers in metal processing, water treatment, food and feed, pharmaceuticals, transport and process manufacturing, as well as power generation, waste-to-energy and cement production.
From process chemistry to NOx reduction in SCR and SNCR systems, we match the product specification, concentration and delivery format to your application. We combine production and sourcing with storage, specialist transport and coordinated deliveries, with stock monitoring and replenishment planning available by agreement.
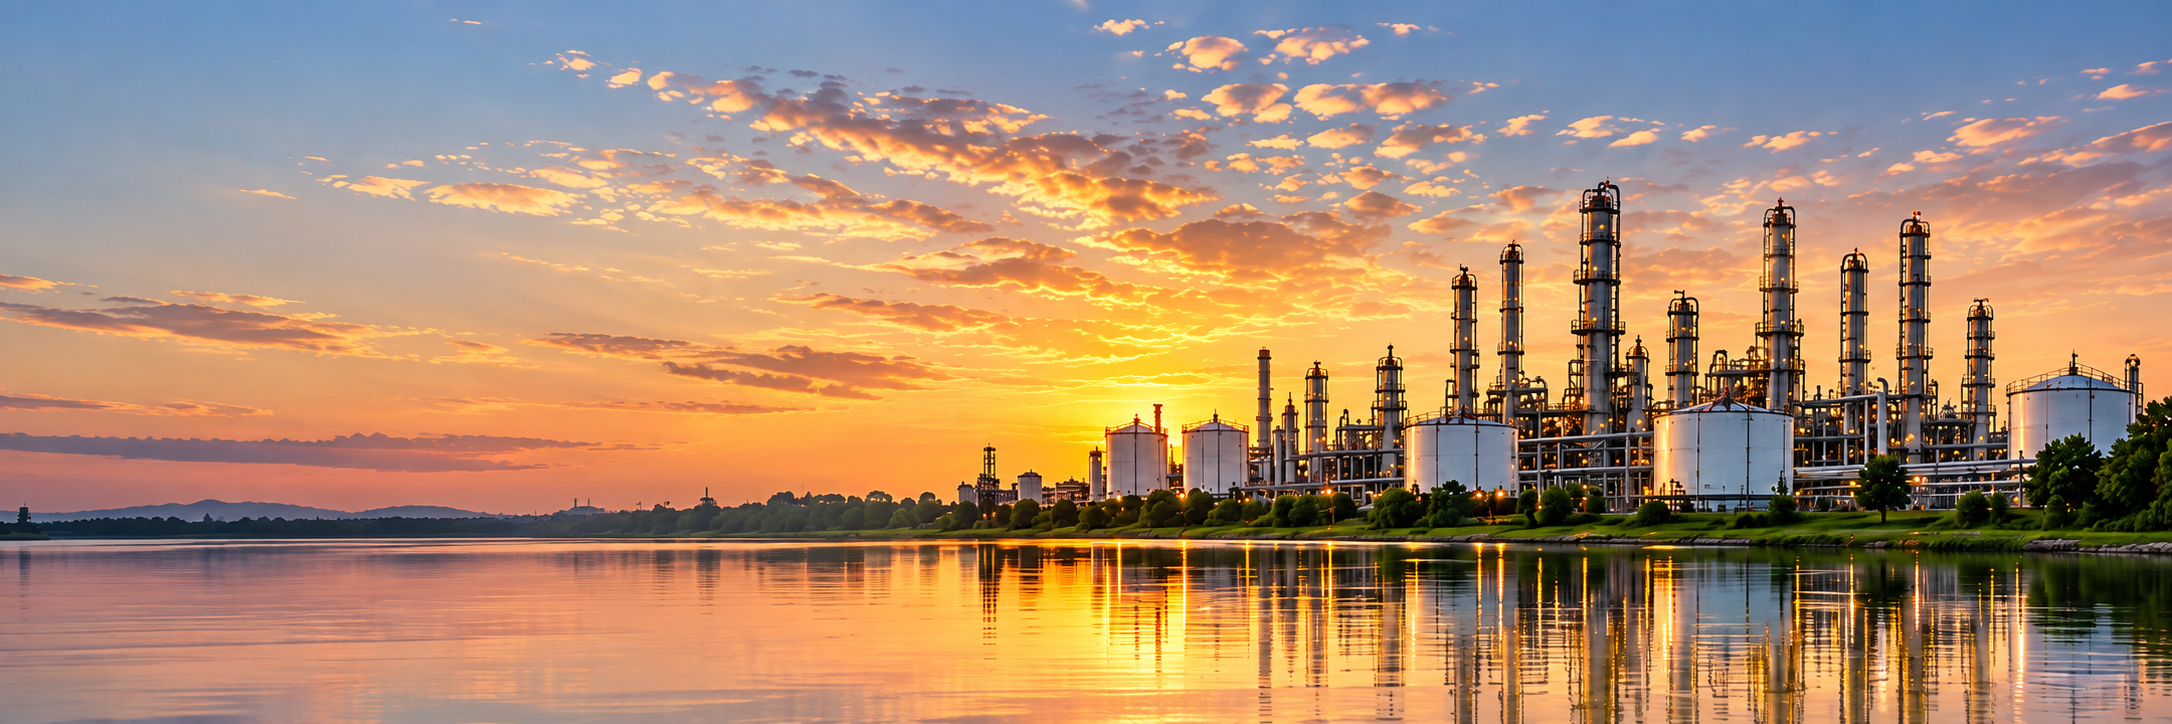
Power plants require controlled water and steam chemistry to protect equipment and support efficient operation. Chemical purity, concentration and supply continuity are key considerations. We match product specifications, delivery schedules and replenishment planning to your plant’s operating requirements.
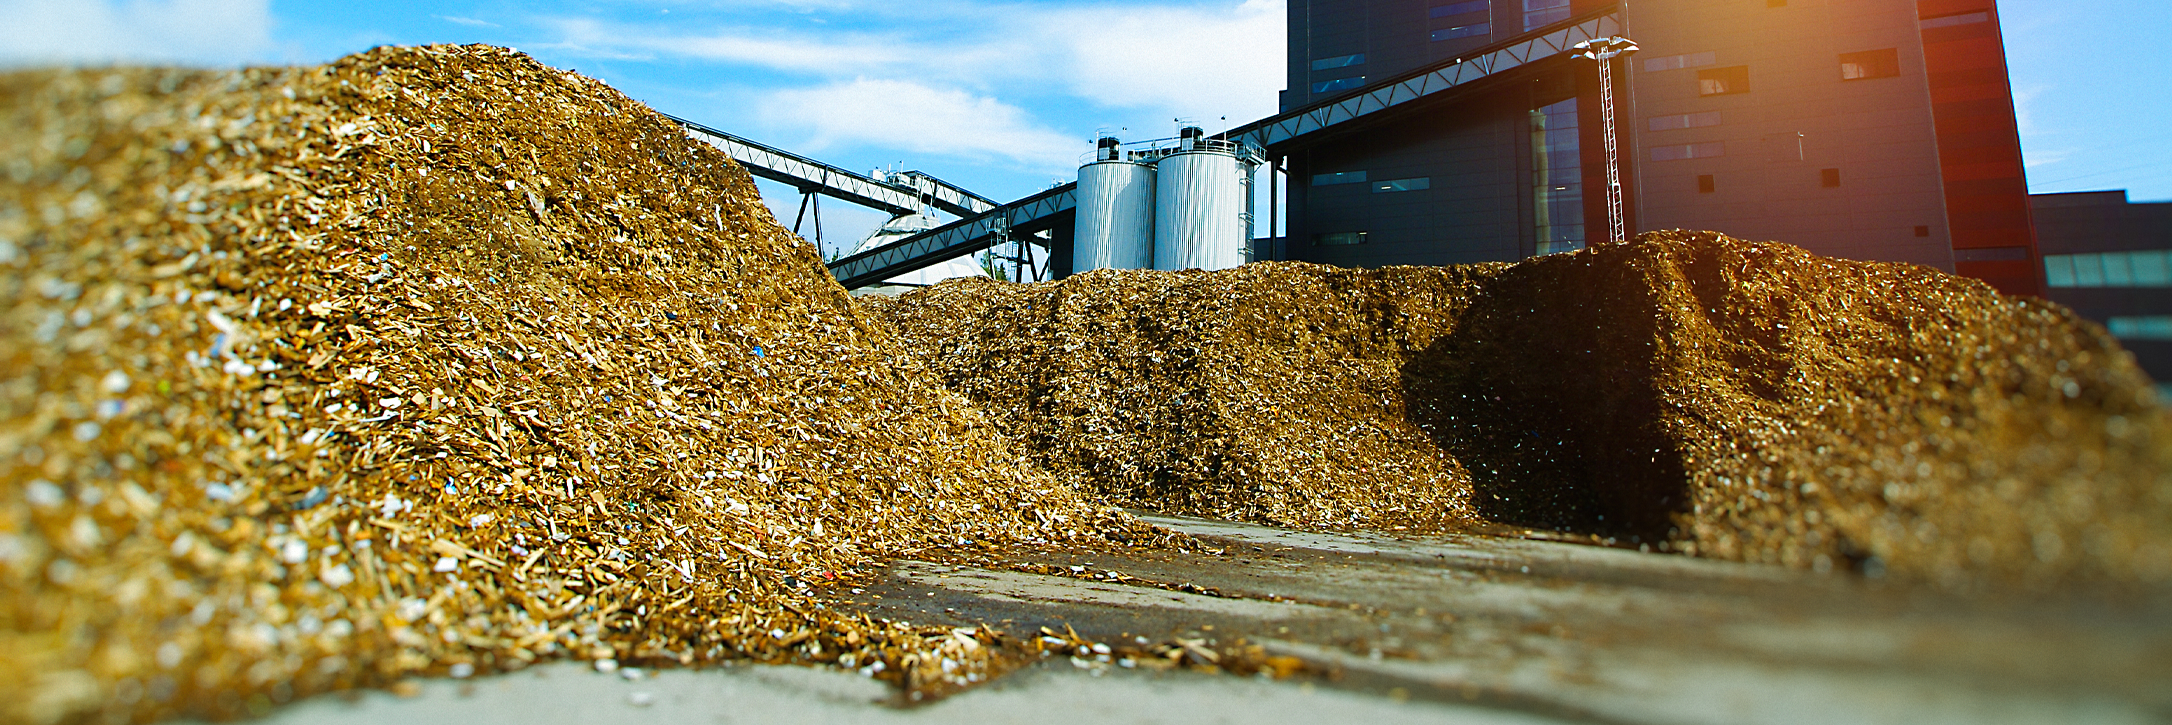
Waste-to-energy plants depend on chemical reagents for flue-gas treatment and water management. Supply planning must account for reagent consumption, storage capacity and delivery access. We coordinate product concentrations, specialist transport and replenishment around your plant’s operating needs.
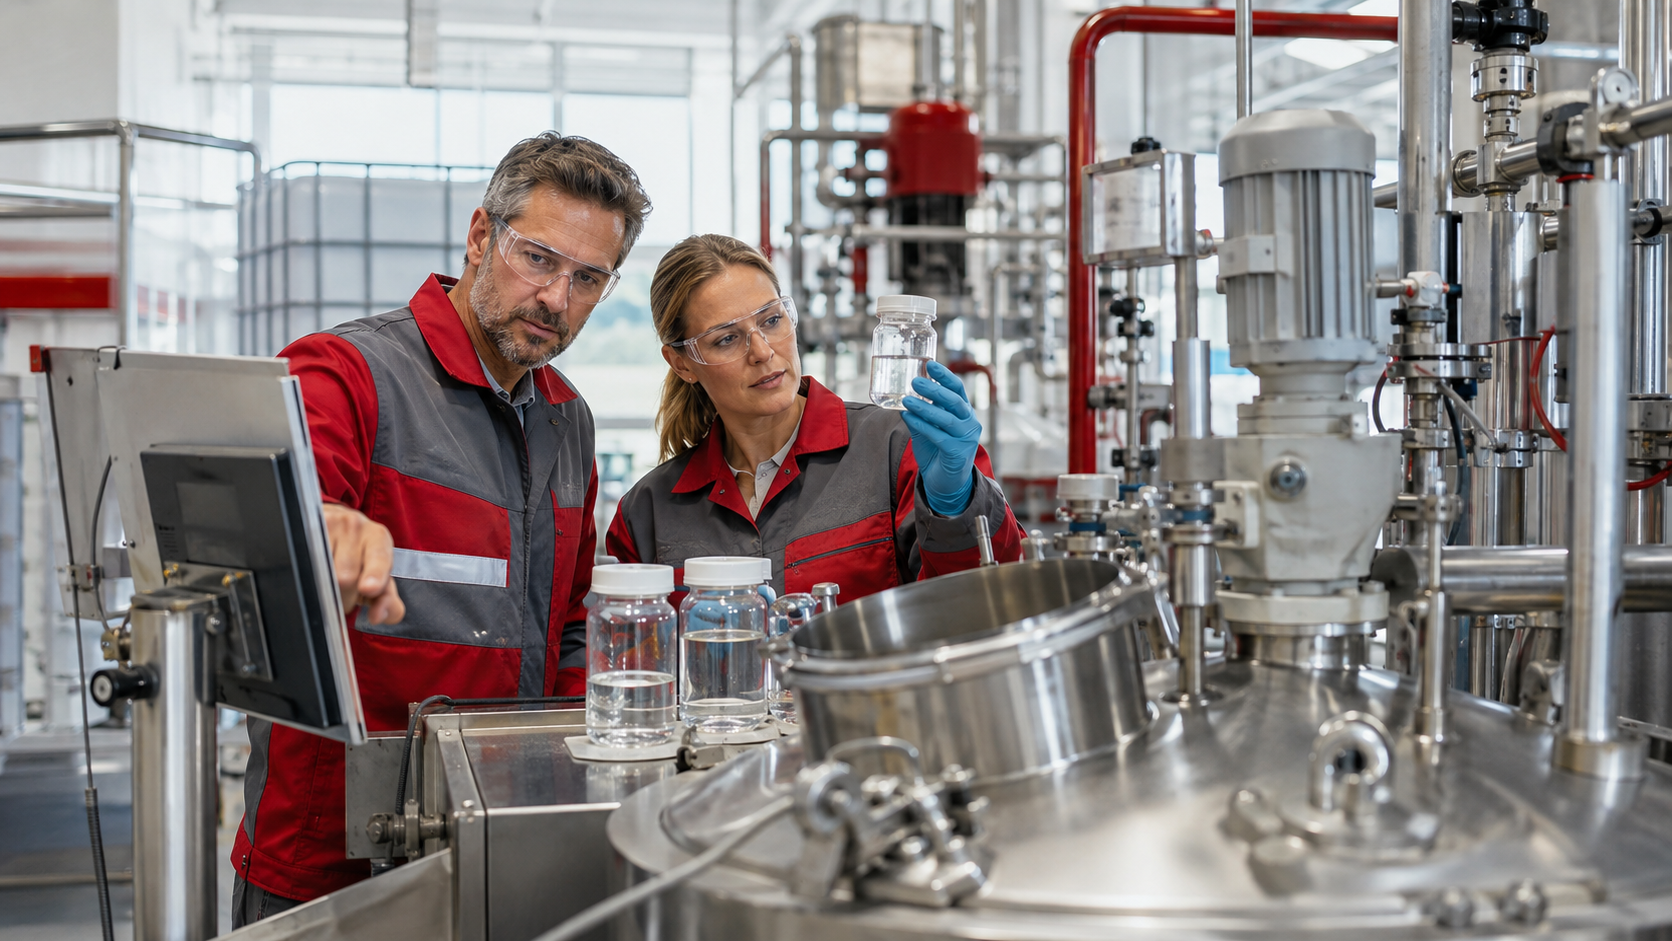
Consistent chemical quality and concentration help manufacturers maintain stable processes and product quality. We combine sourcing with custom dilution, blending and packaging, matching chemical supply to your formulation, consumption and production schedule.
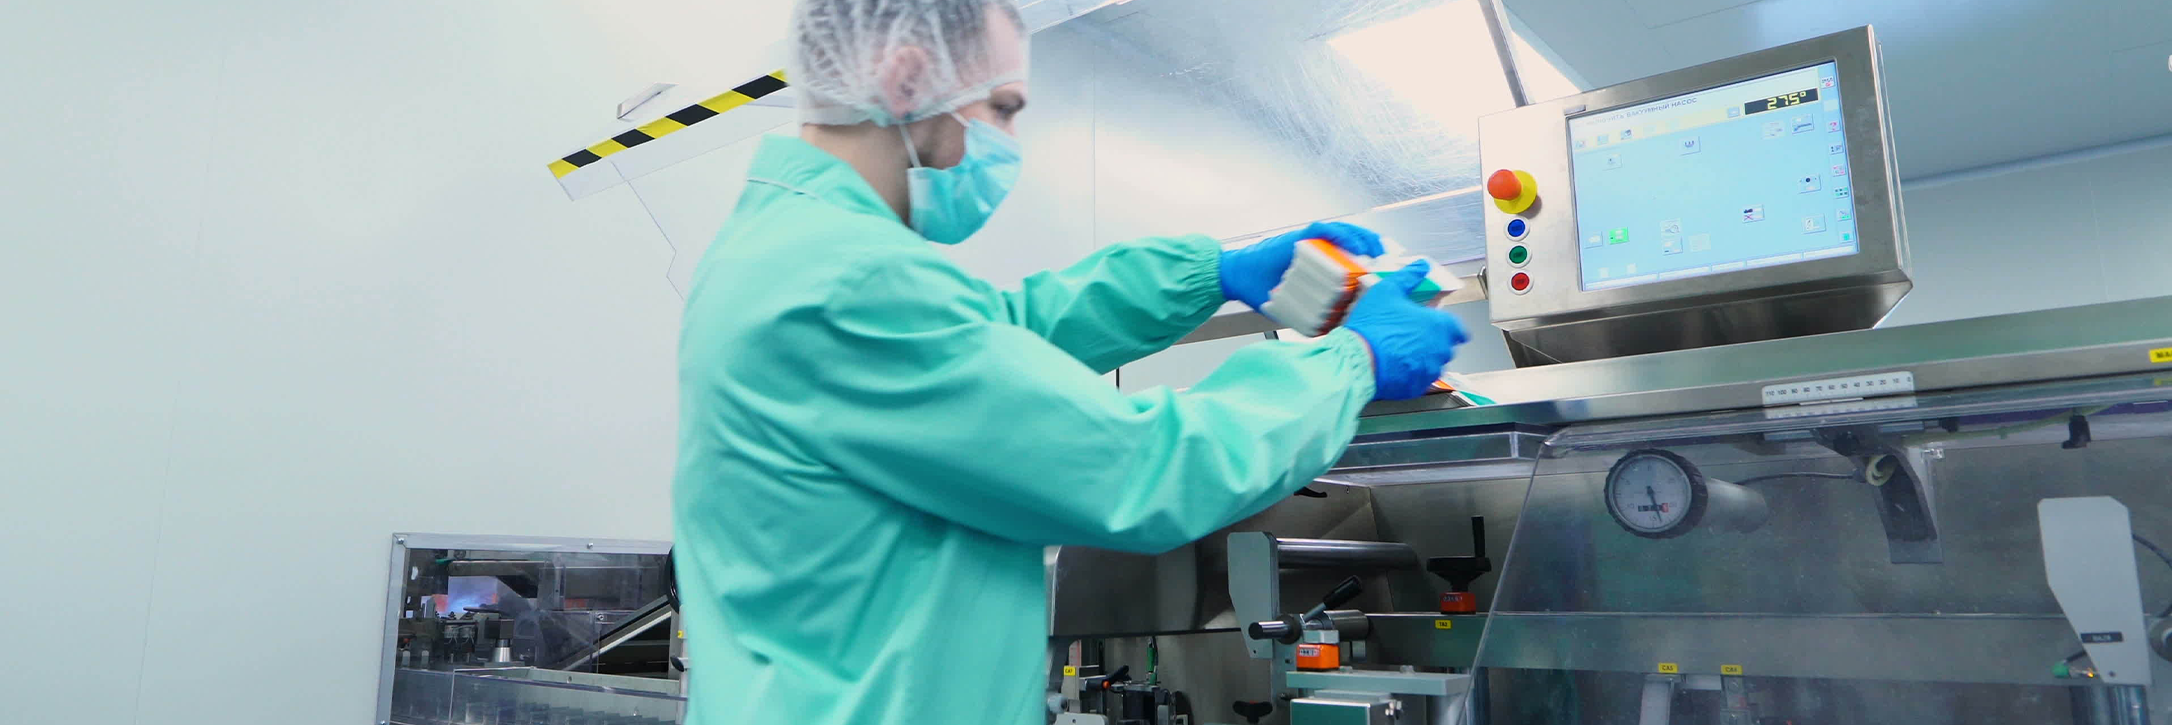
Pharmaceutical manufacturing requires clearly defined specifications, traceability and supporting documentation. We review the intended use, required grade and supplier qualification requirements before proposing a supply arrangement. Packaging, handling and delivery are agreed for the specific application.
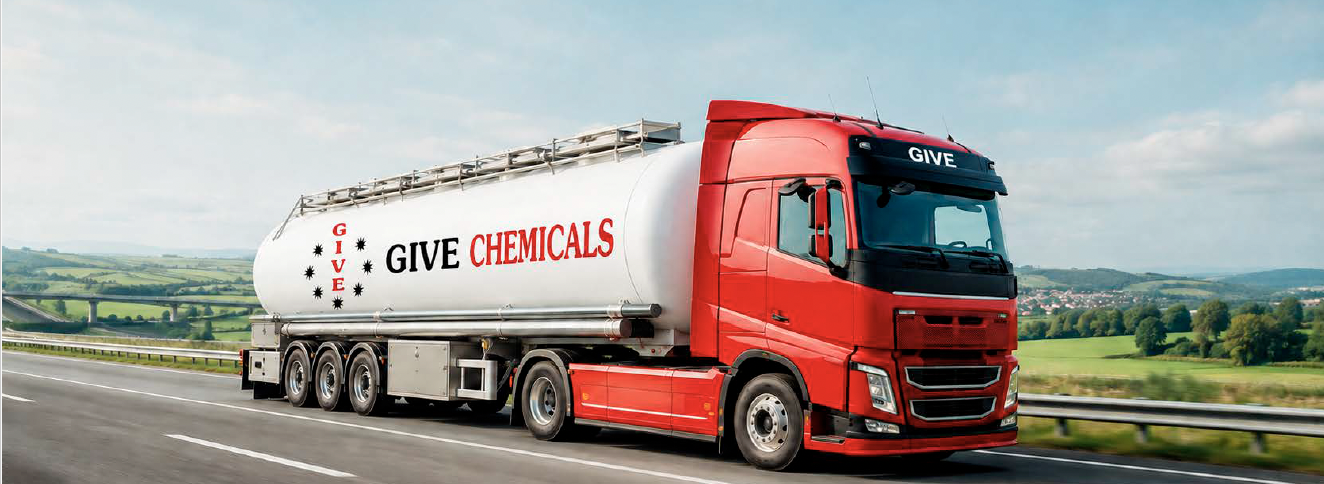
Transport operators need dependable AdBlue supply for vehicles and machinery equipped with SCR systems. Product quality, clean handling and compatible storage are essential. We supply in bulk, IBCs, drums and canisters, with delivery volumes and frequency matched to fleet consumption.
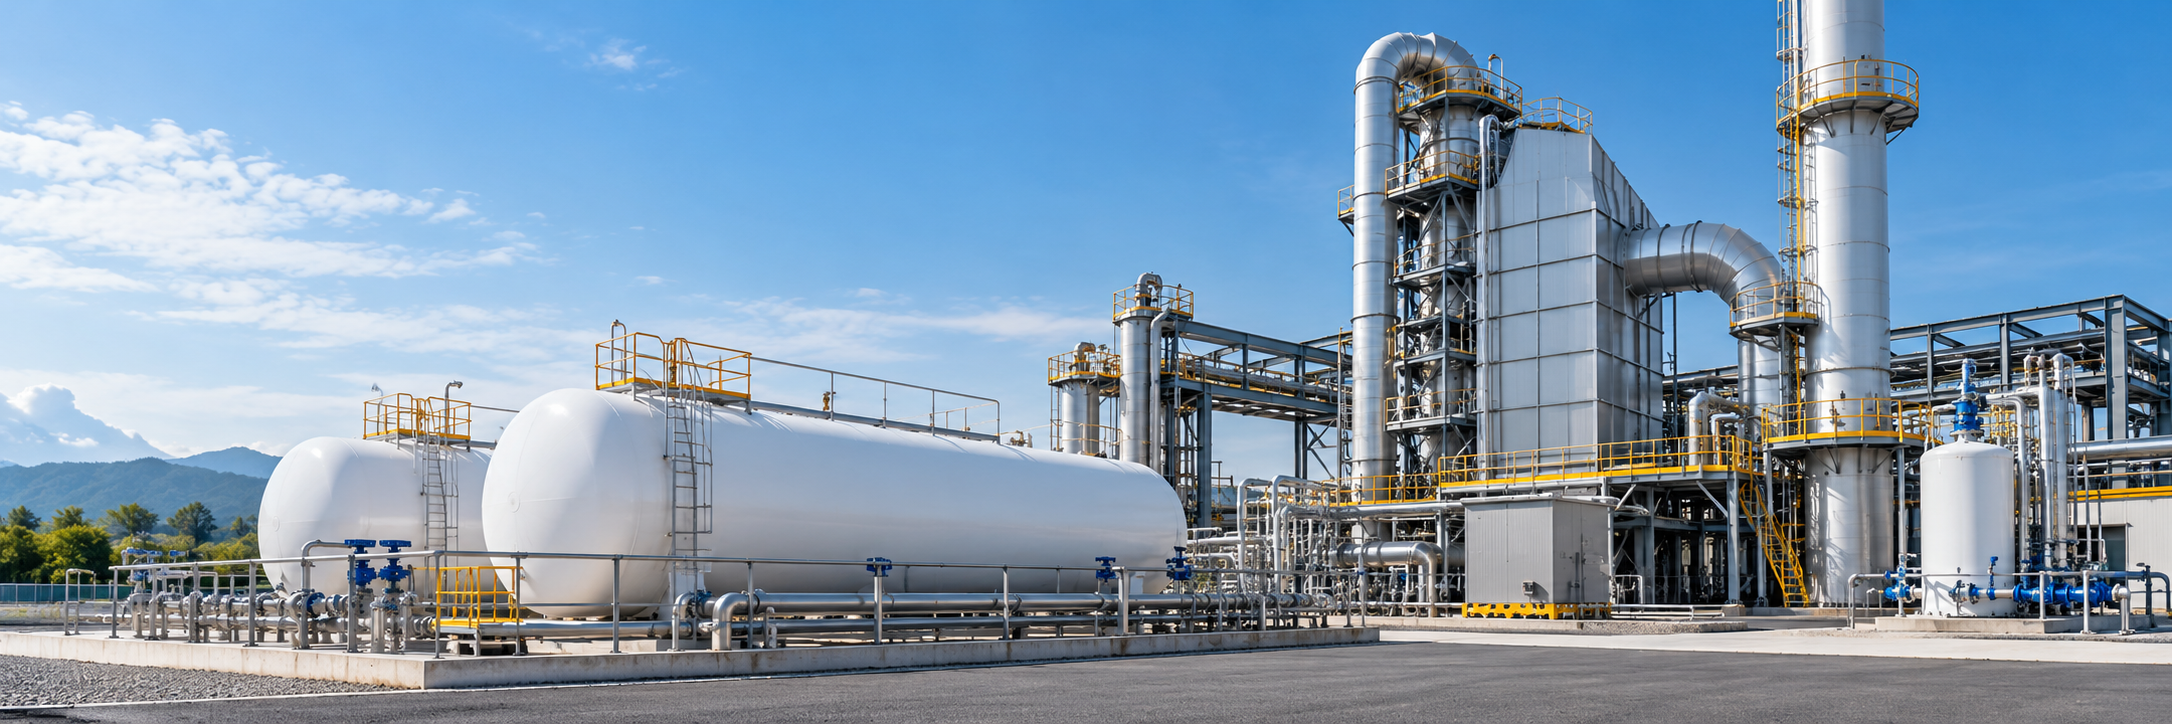
Ammonia and aqueous ammonia are used for NOx reduction in SCR and SNCR systems. Reagent concentration and purity must match the installation’s requirements. We combine product supply with specialist handling, distribution and replenishment planning, with stock monitoring available by agreement.
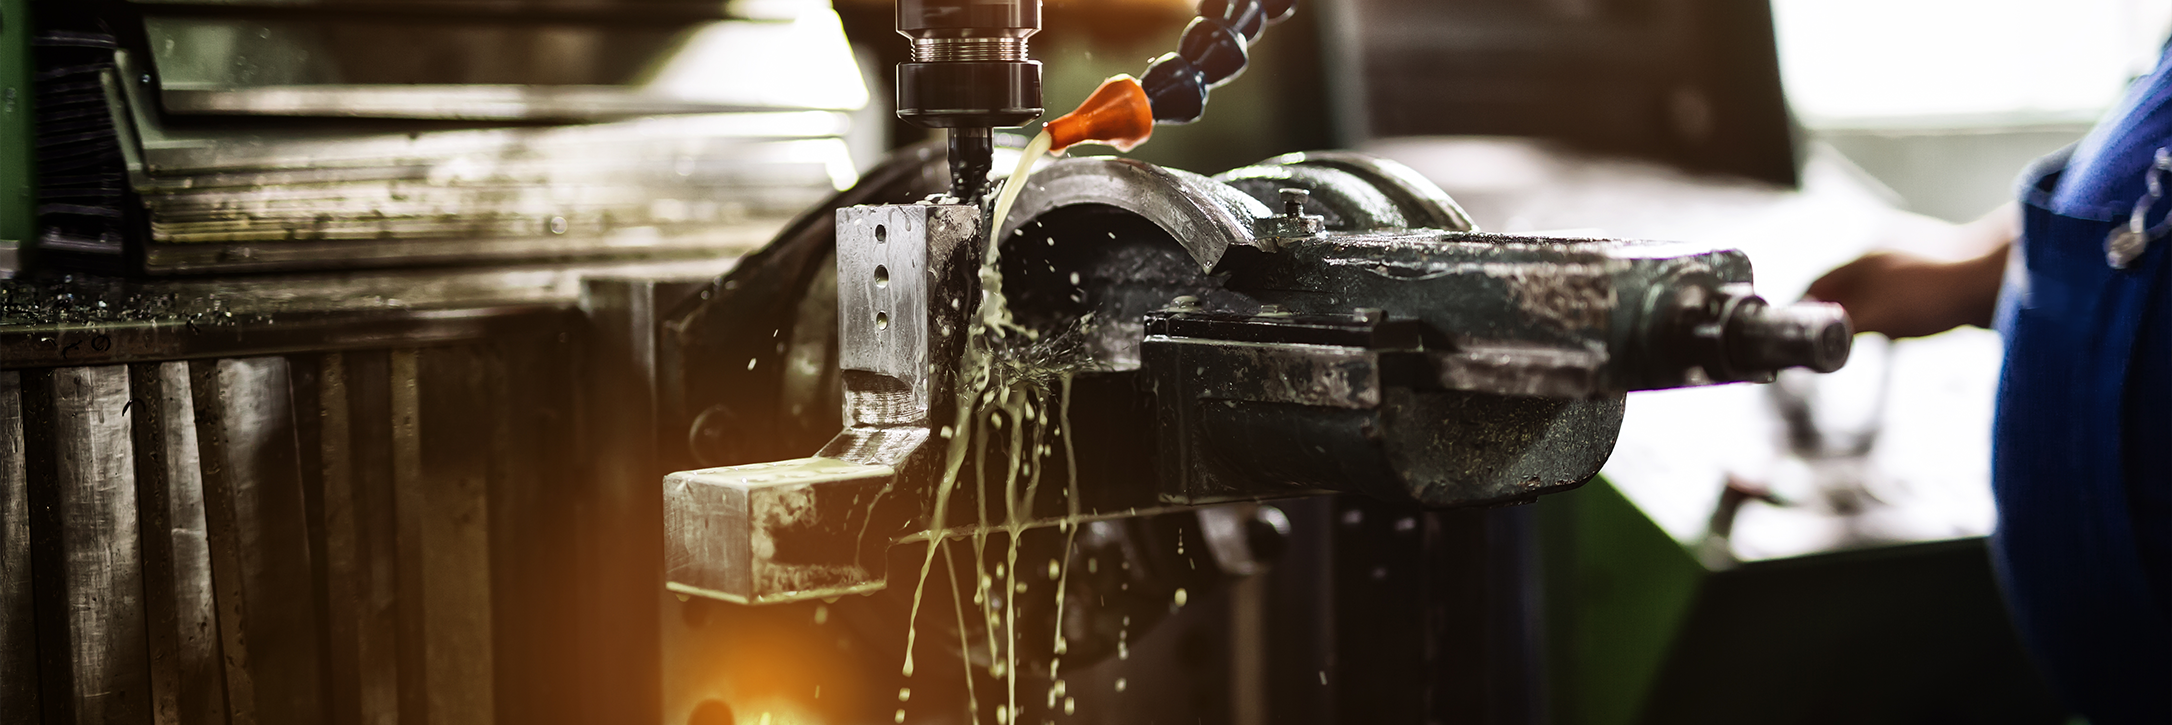
Metal processing uses chemicals for cleaning, pickling and surface treatment. Concentration, impurity limits and compatibility with the metal being treated influence process performance and surface quality. We supply acids, alkalis and demineralised water, with specifications and delivery formats matched to your production requirements.
Water and wastewater treatment require chemicals suited to the treatment process, including pH adjustment and neutralisation. Consistent concentration and reliable replenishment support stable operation. We supply acids, alkalis and other agreed treatment chemicals, with quantities and delivery formats matched to your consumption and receiving facilities.
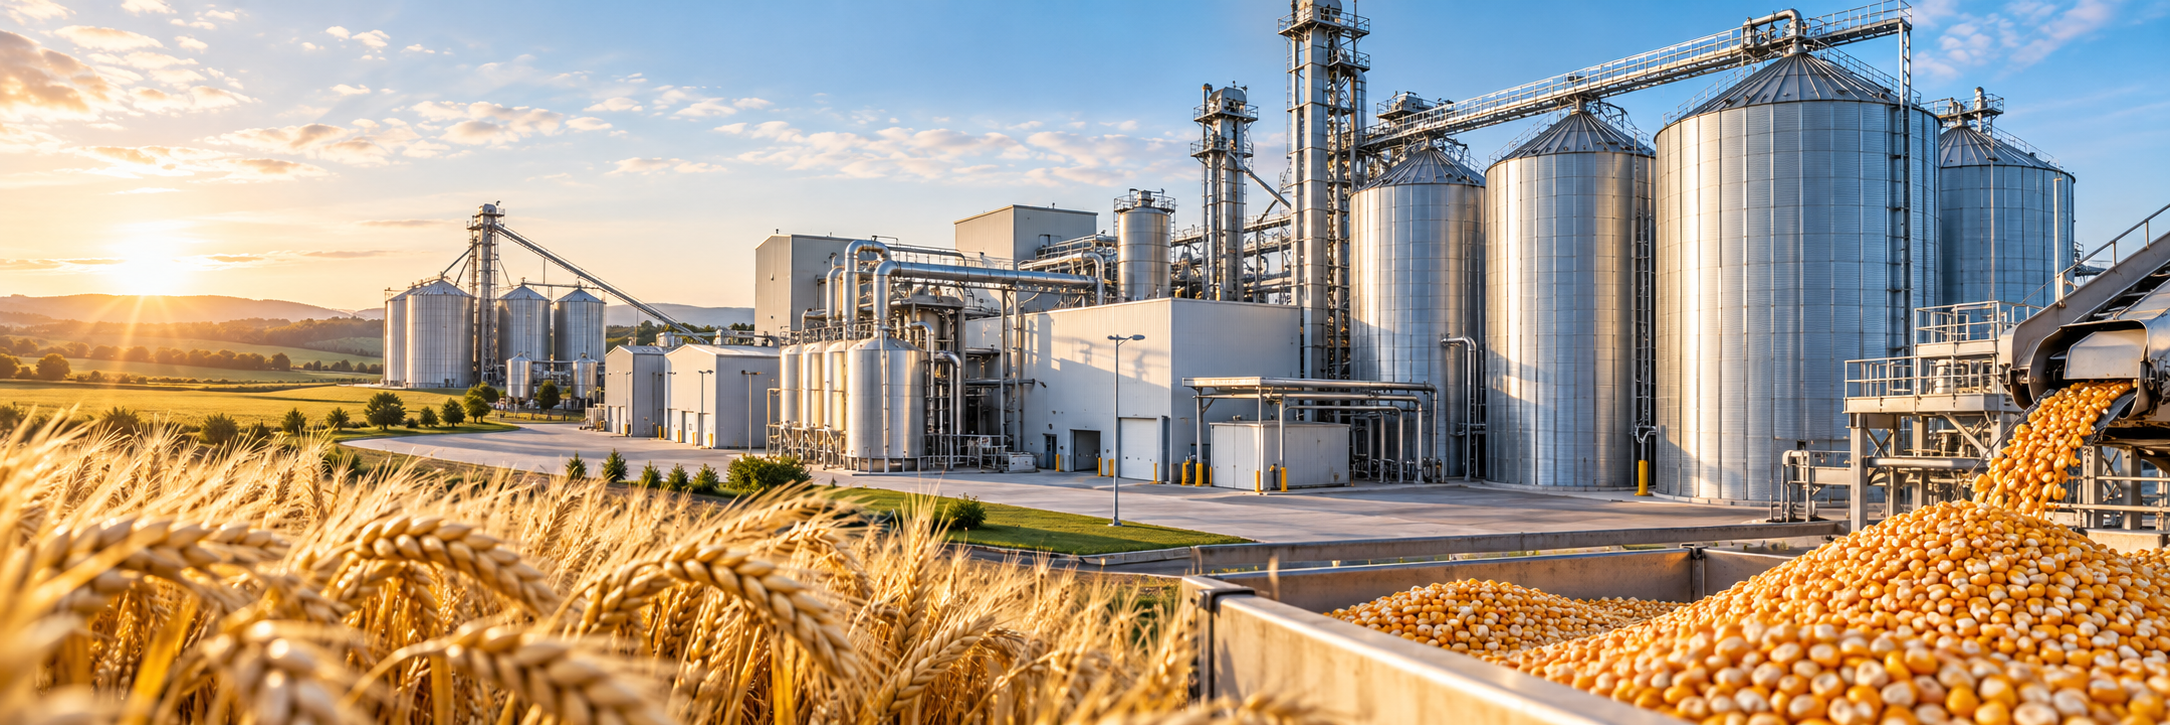
Food and feed production requires clear product specifications, appropriate grades and relevant documentation. We review the chemical, intended use and handling requirements before agreeing supply. Bulk and packaged formats are matched to your hygiene requirements, production volumes and receiving facilities.
Industrial refrigeration
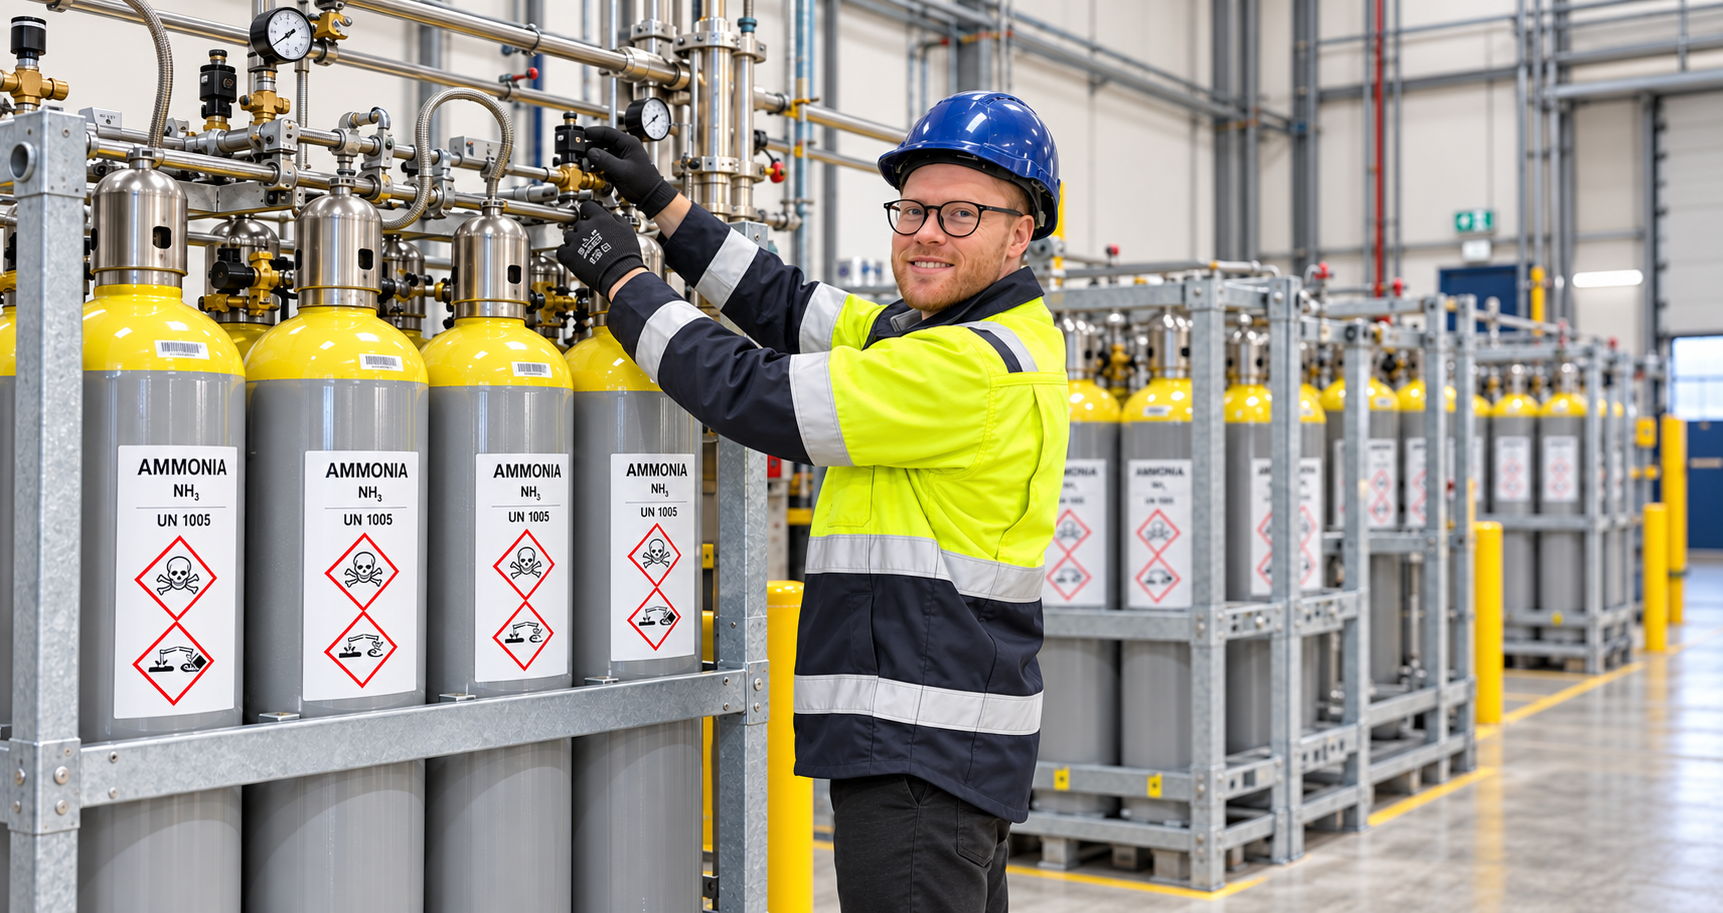
Our high-purity ammonia project is being developed for future R717 and HP Ammonia 99,99 (N4) supply. Start-up is expected at the end of 2026; suitability for each installation will depend on its specification and equipment-manufacturer requirements.
Ammonia is an established natural refrigerant for cold stores, food-processing plants, ice production and other industrial cooling installations. R717 has zero ozone-depletion potential and zero direct global-warming potential.
For refrigeration enquiries, purity is considered together with water, oil and non-condensable gas limits. The installation's requirements and the equipment manufacturer's specification determine the acceptable refrigerant quality.
Products | Sourcing | Safety & Quality
Connect product specification with everyday use.
A chemical supply arrangement needs to fit how a product is received, stored and used in your process. Our core portfolio and customer-specific sourcing can be combined with dilution, blending and packaging where appropriate.
Product sourcing
Specification matching
Custom concentrations
Dilution planning
Customer-specific blending
Bulk supply
Packaged chemicals
Receiving-site compatibility
Storage coordination
Distribution planning
Delivery scheduling
Stock monitoring
Specialist ammonia handling
Acid and caustic supply
Supply arrangement review
Products | Dilution and blending | Packaging
Tell us what your site needs
Discuss your chemical supply requirements
Contact Give Chemicals with your application, product specification, site requirements and expected volumes. Tell us how you receive and use the product, and our team can discuss suitable sourcing, preparation, packaging and delivery arrangements. Use our contact form to start the conversation.
GIVE CHEMICALS
Industrial chemical supply, custom processing, packaging and specialist logistics.
WE HANDLE · WE CREATE · WE DELIVER
CONTACT
Give Chemicals ApS
Hjortsvangen 26
DK-7323 Give, Denmark
+45 76 70 15 00
VAT: DK30592271
- Products
- Solutions
- Industries
- Safety & Quality
- About
- Contact